Why Transformer Core Quality Matters to Global Buyers?
For global buyers, transformer core quality is not a minor specification. It affects energy efficiency, operating temperature, noise, service life, and total ownership cost. A well-made Transformer Core can reduce magnetic losses during continuous operation. This matters in substations, renewable energy projects, factories, and commercial buildings. Even a small efficiency difference can become significant after thousands of operating hours.
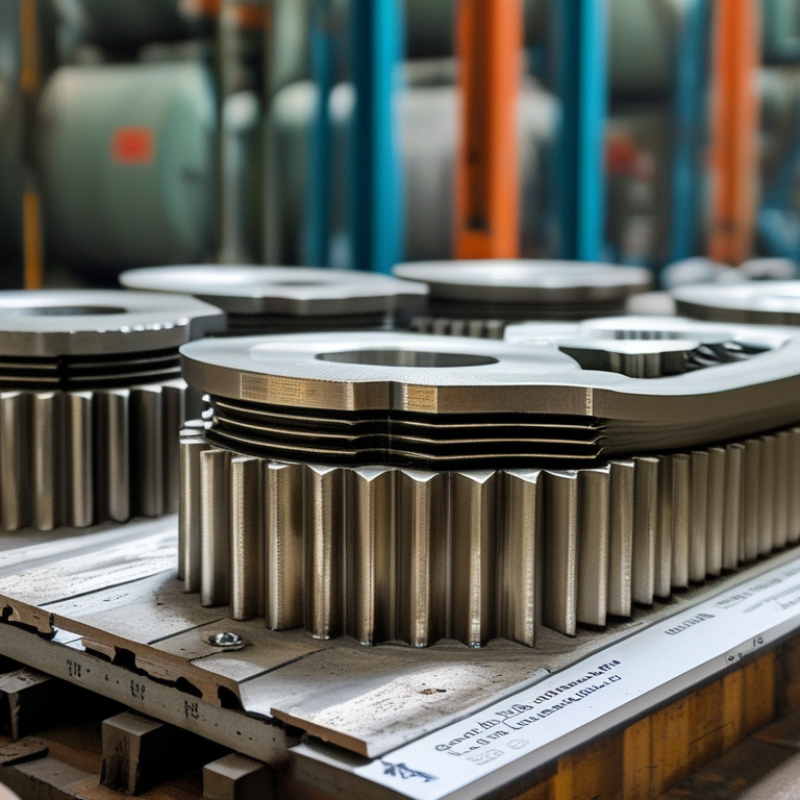
Experienced procurement teams inspect more than datasheets. They review steel grade, lamination thickness, burr control, joint design, stacking accuracy, and manufacturing traceability. They may also request loss measurements, dimensional records, inspection reports, and independent test results. These details reveal whether a supplier controls production consistently or simply describes ideal performance. A core that looks precise in photographs may still show uneven clamping or excessive gaps during inspection. That is where practical judgment matters.
Quality is not always easy to compare.
International buyers must consider climate, voltage requirements, transport conditions, and local maintenance capability. A design suitable for one grid may perform poorly in another application. Certifications provide useful evidence, but they do not replace factory audits or technical communication. This point is often underestimated. Reliable suppliers explain limitations clearly and support claims with verifiable data. They also acknowledge possible variation instead of promising perfection. Buyers should therefore evaluate the Transformer Core as part of the complete transformer system, not as an isolated component. Careful comparison can protect efficiency, reliability, and long-term project value.
Why Transformer Core Quality Matters to Global Buyers?
Transformer Core Basics: Grain-Oriented Steel and 50/60 Hz Operation
Grain-oriented electrical steel guides magnetic flux through aligned crystal directions. This structure reduces hysteresis and eddy-current losses. At 50 or 60 Hz, core design must match the rated frequency precisely. A 60 Hz core operated at 50 Hz may experience higher flux density. That can increase noise, heating, and no-load losses. IEC 60076-1 defines key transformer performance requirements, while IEC 60404-8-7 classifies grain-oriented electrical steel grades.
Core quality becomes visible during testing. Poor cutting can damage the steel’s magnetic path. Small burrs may create local circulating currents. Excessive clamping pressure can also increase losses. Industry datasheets commonly report specific losses near 0.9–1.3 W/kg at 1.7 tesla and 50 Hz, depending on grade and processing. The U.S. Department of Energy’s transformer efficiency analysis shows that no-load losses remain important throughout a transformer’s service life. The International Energy Agency reported that global grid investment must exceed 600 billion dollars annually by 2030. Efficient cores therefore support both operating savings and grid expansion.
Tips: Ask for loss data at the actual frequency and flux density. Check test methods, cutting quality, stacking factor, and audible-noise results. Do not compare values from different test conditions. A lower advertised loss may not mean better field performance. Buyers should also review sample test records, though one factory sample cannot prove long-term consistency. That limitation deserves attention.
For global transformer buyers, core quality starts with a measurable question: how much power becomes heat? W/kg at 1.7 T offers a practical comparison point for electrical steel. Under IEC 60404-8-4, laboratories assess specified material conditions using controlled test methods. The reported value can expose differences that appearance cannot.
A lower W/kg usually means lower no-load losses in service. However, the number is meaningful only when test conditions match. Buyers should check frequency, waveform, specimen direction, thickness, coating, and stress relief. They should also confirm whether results come from an Epstein frame or another permitted method. Small changes can alter the reading. Request the test date, sample identification, and calibration records. Traceability matters.
Factory experience shows another issue. Material tested in a laboratory may perform differently after cutting and assembly. Burrs, bending, joints, and clamping pressure can increase actual losses. This is why acceptance plans should connect sheet data with assembled-core tests. A single W/kg figure is not enough. It is a useful signal, not a complete verdict. Buyers should compare uncertainty, sampling frequency, and corrective-action procedures alongside the headline metric. Some specifications remain imperfect. That is worth admitting. Reliable sourcing depends on transparent evidence, repeatable testing, and engineers willing to question attractive numbers.
A transformer core works continuously, even when its load is light. The U.S. Department of Energy’s 2024 Distribution Transformer Energy Conservation Standards Technical Support Document evaluates losses across a 30-year service life. That long horizon makes small no-load losses commercially important. Core steel thickness directly affects eddy-current loss. Under similar magnetic conditions, eddy losses approximately follow the square of lamination thickness. Moving from 0.27 mm to 0.23 mm steel could reduce this component by about 27.5%.
The number is useful. It is not a guarantee. IEC 60404-2 testing shows that steel grade, coating, frequency, and magnetic flux density also influence measured core loss. A 0.23 mm sheet can perform poorly if its edges contain burrs. Tight bends create local circulating currents. Poor cutting may also increase joint losses.
During factory checks, buyers should request loss data at the specified flux density, not only a catalog value. Inspect stacking factor, burr height, insulation coating, and mitered joints. The core should feel uniform under inspection, with no visible damage at corners. CIGRE technical guidance repeatedly treats design, manufacturing, and operating conditions as connected variables. That matches practical experience. I have seen excellent steel lose its advantage after careless assembly. Thin laminations help, but workmanship decides whether the specification becomes real performance.
For global buyers, transformer core quality is not an abstract engineering promise. It appears in small manufacturing details. During factory inspections, I have seen a thin burr along a cut edge. It can damage insulation and increase local losses. Burr height should be checked with calibrated gauges, not judged by touch alone. Inspection records should identify the operator, batch, and measurement time. A clean report does not always mean a clean core.
Stacking factor also deserves close attention. It shows how effectively steel laminations form the magnetic path. Poor alignment, coating damage, or excessive pressure can reduce the active steel area. Buyers should request test results, sampling methods, and the calculation formula.
Joint gaps need equal discipline. Uneven gaps can raise reluctance and create uneven flux distribution. A small opening at a corner may look harmless, yet it can affect noise and temperature. Tolerance limits should be agreed before production, not negotiated after delivery.
Tips: Check burrs under strong side lighting. Measure stacking factor from representative samples. Use feeler gauges for joint gaps. Keep photos with the inspection report. Ask for corrective-action records when results miss target values. No inspection is perfect. Repeated sampling remains necessary, especially when tooling changes. My own preference is to combine factory measurements with independent verification, because numbers without context can still mislead.
Why Transformer Core Quality Matters to Global Buyers?
A transformer core controls no-load loss, excitation current, and operating temperature. Poor steel selection or uneven clamping can increase losses and audible noise. During buyer verification, request test evidence aligned with IEC 60076 and IEEE C57.12.90. These standards provide recognized methods for measuring no-load loss and excitation current. Test records should state voltage, frequency, temperature, tap position, and instrument accuracy. Without these details, a number has limited value.
In factory inspections, buyers should compare measured results with the approved design and contractual limits. Check whether the core is properly grounded, insulated from the frame, and free from visible burrs or damaged laminations. A low no-load loss reading alone does not prove excellent core construction. Test equipment may be poorly maintained, or the measurement setup may be incomplete. That possibility deserves attention. Ask for calibration certificates, raw readings, test dates, and corrective-action records. Independent witnessing can add credibility when project risks are high.
Tips: Request repeat measurements when results look unusually good. Confirm the test frequency matches the transformer rating. Review trends across production units, not one attractive report. Small inconsistencies may reveal process weakness before field installation. Test reports should be clear enough for an engineer outside the factory to verify.
| Verification Dimension | Core-Related Test or Review | Relevant Standard Reference | Measured Data and Units | What the Result Indicates | Buyer Verification Evidence |
|---|---|---|---|---|---|
| No-load performance | No-load loss test | IEC 60076-1; IEEE C57.12.90 | Core loss in W or kW; applied voltage in V or kV; frequency in Hz; energized phase or winding connection | Assesses the magnetic core’s operating loss at rated voltage and frequency. Excessive loss may indicate unsuitable electrical steel, poor joint quality, incorrect flux density, or manufacturing damage. | Routine or type-test report showing calibrated instruments, test frequency, applied voltage, temperature, connection diagram, corrections, and recorded loss values. |
| Excitation behavior | Excitation-current measurement | IEC 60076-1; IEEE C57.12.90 | Excitation current in A or percentage of rated current; test voltage and frequency; current by phase where applicable | Helps identify abnormal magnetic saturation, localized core damage, excessive joint air gaps, or winding and connection issues affecting the magnetic circuit. | Phase-by-phase or line-to-line readings, test conditions, instrument accuracy, and comparison with the approved design or factory baseline. |
| Magnetic flux consistency | Voltage-to-frequency verification | IEC 60076-1; IEEE C57.12.90 | Applied voltage in V; frequency in Hz; V/Hz value; waveform information when recorded | Confirms that the core is tested at the specified magnetic flux level. A higher-than-intended V/Hz ratio can drive the core toward saturation and distort loss results. | Test sheet stating rated frequency, actual frequency, applied voltage, test sequence, and any voltage or frequency correction used. |
| Core assembly quality | Visual and dimensional inspection of laminations, joints, clamps, and core grounding | IEC 60076-1; purchaser’s approved drawings and inspection plan | Core window and limb dimensions in mm; lamination condition; joint configuration; grounding arrangement; visible burrs, gaps, and coating damage | Reveals assembly conditions that can increase localized flux concentration, circulating currents, vibration, acoustic noise, and no-load loss. | Inspection checklist, dimensional records, photographs, approved drawings, material traceability, and nonconformance disposition records. |
| Core insulation integrity | Core-to-ground insulation and core-grounding arrangement review | IEC 60076-1; project specification and approved manufacturer test procedure | Insulation resistance in MΩ when specified; test voltage and duration; grounding lead continuity; number of intentional grounding points | Checks that the core is intentionally grounded at the designated point and that unintended parallel current paths are not present. | Recorded resistance or continuity results, grounding schematic, physical inspection record, and confirmation that temporary shipping grounds were removed or documented. |
| Loss verification | Load-loss and impedance test as a complementary check | IEC 60076-1; IEEE C57.12.90 | Load loss in W or kW; short-circuit impedance in %; test current in A; reference temperature in °C | Primarily evaluates winding and leakage-flux performance, but abnormal results can help identify mechanical displacement, stray-loss concerns, or test-configuration errors that should not be attributed to the core alone. | Test report with corrected values, reference temperature, tap position, current, voltage, impedance, and separation of load loss from no-load loss. |
| Electrical ratio confirmation | Transformer turns-ratio, polarity, and phase-relation tests | IEC 60076-1; IEEE C57.12.90 | Measured ratio; percentage deviation from specified ratio; polarity or phase displacement; tap position | Confirms that the magnetic circuit and winding connections produce the intended voltage relationship. An incorrect ratio can invalidate comparisons of no-load current and loss. | Ratio-test record for every phase and tap position, instrument calibration certificate, vector-group or phase-relation confirmation, and approved nameplate data. |
| Dielectric coordination | Applied-voltage and induced-voltage insulation tests | IEC 60076-3; IEEE C57.12.90 | Test voltage in kV; test duration in s; frequency in Hz; leakage or discharge observations where applicable | These are insulation-system tests rather than direct core-loss tests. They help verify that core, windings, insulation structures, and clearances withstand the specified electrical stresses. | Type or routine test report identifying test connections, test levels, duration, frequency, environmental conditions, and pass/fail observations. |
| Thermal and mechanical behavior | Temperature-rise and sound-level review when specified | IEC 60076-2; IEC 60076-10; IEEE C57.12.90 | Top-oil and winding temperature rise in K; ambient temperature in °C; sound pressure level in dB(A); test load and distance | Unexpected temperature or acoustic behavior can be associated with excessive core loss, core clamping issues, magnetostriction, or structural resonance, although root-cause analysis is required. | Type-test report, test layout, ambient conditions, load current, sound-measurement locations, temperature readings, and stated measurement uncertainty. |
| Data integrity and acceptance | Independent review of test method, calibration, and contractual limits | IEC 60076 series; IEEE C57.12.90; purchaser’s technical specification | Instrument accuracy; calibration date; uncertainty; stated tolerances; measured value versus guaranteed value; deviations in % | Standards define test methods and reporting principles, while guaranteed losses, impedance tolerances, acceptance limits, and retest rules are normally established by the purchase contract or approved specification. | Signed test dossier, calibration certificates, raw data, calculation sheets, deviation list, approved test plan, and witness or third-party inspection records where required. |
| Buyer note: IEC 60076 and IEEE C57.12.90 provide standardized test procedures, but they do not create one universal pass/fail value for every transformer design. Acceptance should be based on the transformer rating, voltage class, frequency, design guarantees, specified tolerances, and the purchaser’s approved technical requirements. | |||||